Services
Top Dual Energy Inspection Systems for Global Buyers
Global buyers are investing in smarter inspection as passenger volumes, parcel traffic, and supply-chain complexity continue to rise. IATA’s 2024 passenger data shows a strong recovery in global air travel, increasing pressure on airports and logistics hubs. This growth makes reliable screening equipment more important. Dual Energy Inspection systems help operators distinguish materials by estimating effective atomic number and density. A dense suitcase appears differently from an organic-rich package.
The technology is not a magic solution.
The World Customs Organization’s SAFE Framework emphasizes risk management, secure trade, and cooperation between border agencies. These principles matter when selecting equipment for airports, customs facilities, warehouses, and transport terminals. Buyers should examine image quality, conveyor speed, tunnel dimensions, software integration, operator training, and maintenance support. Radiation safety must also follow applicable national requirements and recognized international guidance, including recommendations from the International Atomic Energy Agency.
Market reports from organizations such as MarketsandMarkets and Grand View Research indicate continued expansion in security inspection and cargo-screening technologies. However, forecasts are not guarantees. Regional budgets, certification rules, climate conditions, and local service capacity can change the buying decision.
A practical evaluation should include real test bags, mixed-density objects, fragile electronics, folded clothing, and tightly packed cartons. Vendor demonstrations can look impressive. Field performance may differ.
The best system is not always the most expensive one. Global buyers need verified detection performance, transparent specifications, dependable after-sales service, and measurable total ownership costs. This guide compares leading Dual Energy Inspection systems through those practical and professional criteria.
What Dual Energy Inspection Systems Are
Top Dual Energy Inspection Systems for Global Buyers
What Dual Energy Inspection Systems Are
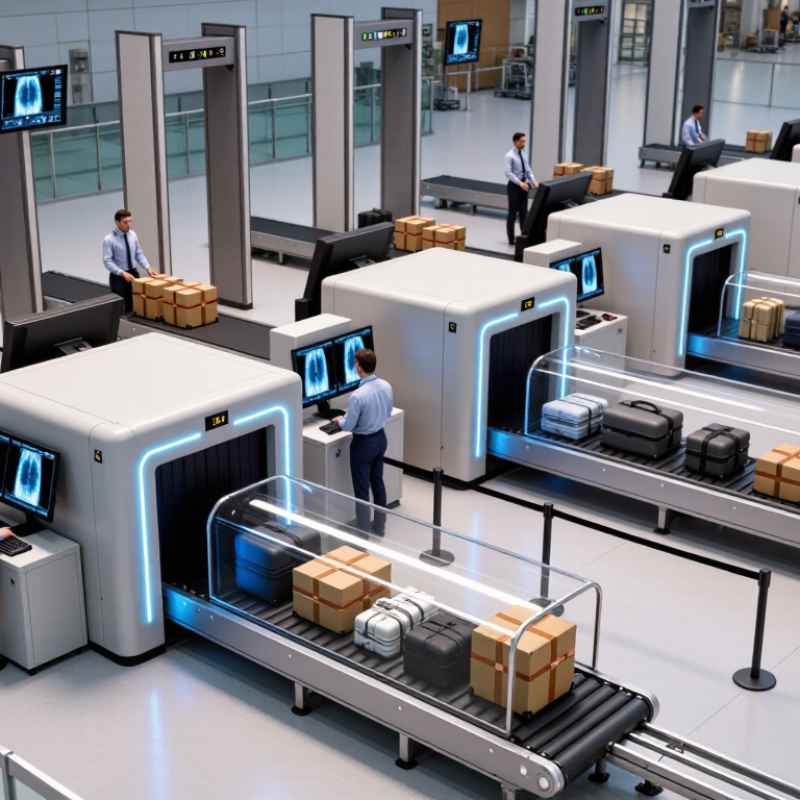
Dual energy inspection systems use two X-ray energy levels to examine an item. Each level interacts differently with materials, depending on density and atomic composition. Software compares these signals and creates a clearer material-based image.
A standard X-ray image mainly shows thickness and overall absorption. Dual energy imaging adds separation between organic, inorganic, and metallic materials. On a conveyor, an operator may see a dense component in one color and a lighter material in another. This visual contrast can make hidden inclusions easier to assess.
The system normally includes an X-ray source, detector array, processing software, and safety shielding. Reliable performance depends on calibration, belt speed, image resolution, and product spacing. Even a strong system can produce uncertain results when products overlap or contain unusual packaging. That limitation matters.
Experienced inspection teams review test samples under real operating conditions. They check whether the system detects small density changes without creating excessive false alarms. Settings should also match local safety rules and workplace procedures. Maintenance logs, operator training, and routine verification support dependable results.
Some materials still resemble each other under dual energy imaging. Moisture, folds, and irregular shapes may confuse the algorithm. Buyers should request application trials, not rely only on brochure specifications. A careful trial often reveals practical weaknesses before installation.
| System Class | Typical Inspection Target | Dual-Energy Principle | Typical Conveyor or Tunnel Format | Material Discrimination | Common Detection Focus | Typical Throughput Range | Key Buyer Evaluation Criteria |
|---|---|---|---|---|---|---|---|
| Food Conveyor X-ray Inspection | Packaged food, frozen products, meat, seafood, bakery products and ready meals | Uses two X-ray energy levels to compare material absorption and improve separation between organic products and dense foreign materials | Sanitary conveyor with a compact inspection tunnel; product spacing and shielding are designed for continuous production lines | Organic vs. inorganic materials | Metal, glass, stone, calcified bone, dense plastic, rubber and missing or broken product components | Usually specified in packs per minute or metres per minute; the actual rate depends on product size, spacing and image-processing time | Hygienic construction, washdown rating, reject accuracy, false-reject rate, line integration and food-safety compliance |
| Parcel and Baggage Inspection | Courier parcels, postal items, cabin baggage and checked baggage | Produces colour-coded or material-classified images that help operators distinguish low-, medium- and high-density contents | Horizontal conveyor tunnel with lead shielding, operator workstation and automatic or manual image review | Effective atomic-number classification | Organic materials, liquids, batteries, electronic devices, dense objects and prohibited items | Commonly designed for continuous belt operation; throughput is determined by conveyor speed, tunnel size and security workflow | Image quality, penetration, threat-detection software, network connectivity, operator ergonomics and applicable aviation or security standards |
| Pallet and Cargo Inspection | Palletized goods, air cargo, freight containers and large commercial shipments | Combines dual-energy imaging with higher-output X-ray generation to classify materials across thicker and more varied loads | Large tunnel or drive-through configuration with reinforced conveyor, cargo handling equipment or vehicle positioning area | Mixed-density cargo classification | Concealed goods, dense inorganic materials, organic substances, voids and inconsistent cargo contents | Usually measured by pallets, vehicles or containers per hour rather than individual products | Penetration capability, scanning speed, radiation safety zone, maximum load dimensions, weather protection and site infrastructure |
| Industrial Inline Inspection | Castings, extrusions, batteries, tyres, composite parts and assembled components | Uses energy-dependent attenuation differences to support automated detection and classification of internal defects | Integrated into a production cell or conveyor line; may use fixed, multi-view or robotic positioning | Density and composition differences | Voids, cracks, inclusions, porosity, foreign material, incorrect assembly and dimensional deviations | Application-specific; cycle time is determined by part geometry, number of views, required resolution and automation level | Spatial resolution, repeatability, inspection coverage, software integration, traceability and compatibility with manufacturing execution systems |
| Security Checkpoint X-ray System | Hand luggage, personal belongings, tools and small containers at controlled access points | Separates material categories in the X-ray image to support rapid operator assessment of suspicious objects | Compact conveyor tunnel with trays, dual-view options or ergonomic inspection tables | Organic and inorganic separation | Blades, firearms, liquids, batteries, dense objects and concealed prohibited articles | Selected according to passenger flow, belt width, tunnel size and the required inspection procedure | Compact footprint, image enhancement, operator training features, alarm management, maintenance access and regulatory approval |
| Research and Laboratory X-ray System | Material samples, powders, biological specimens, electronic assemblies and laboratory test pieces | Acquires images at different energy spectra to estimate material composition or improve contrast between adjacent materials | Enclosed cabinet, sample stage or precision positioning system rather than a high-speed production conveyor | Quantitative material analysis | Layer structure, density variation, contamination, inclusions, sample composition and internal morphology | Batch or sample-based operation; throughput is normally less important than resolution, repeatability and measurement control | Energy range, detector sensitivity, spatial resolution, calibration, software functions, sample size and laboratory safety controls |
| Buyer note: Dual-energy performance is influenced by X-ray voltage, detector design, object thickness, material composition, conveyor speed and image-processing algorithms. Published penetration, resolution and throughput figures should therefore be compared only when the test conditions and product specifications are equivalent. | |||||||